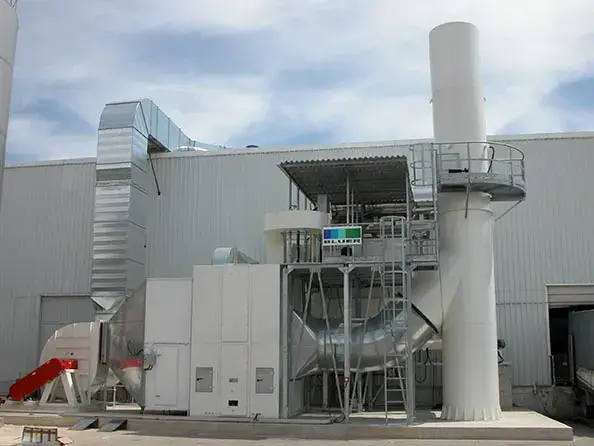
Zeolite concentrators are advanced systems designed for the capture and concentration of VOCs in air streams with low concentrations.
They operate through an adsorption-desorption process, where contaminants are trapped in the zeolite and then released into a more concentrated air stream for further treatment.
This technology reduces operational costs and improves the efficiency of the purification process. At BLUER MEDIOAMBIENTE, we design and implement zeolite concentration systems tailored to each client’s needs.
Zeolite Rotoconcentrator: Efficient Solution for Gas Purification
When the gas flow to be cleaned is high and the concentration of volatile organic compounds (VOCs) is very low (less than 1 g/Nm³), thermal oxidation treatment can be energetically costly. In these cases, concentrating organic compounds into a gas volume up to 16 times smaller is an effective strategy before final treatment.
How the Zeolite Rotoconcentrator Works
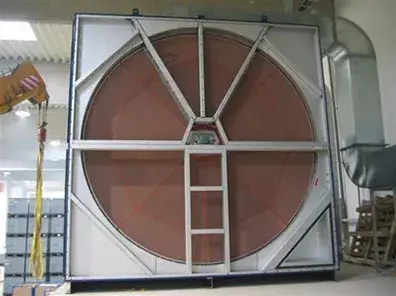
The zeolite rotor concentrator is a device designed to adsorb organic compounds present in the gas stream to be purified. This process is achieved by a zeolite adsorbent impregnated into a corrugated mineral fiber substrate within the rotor.
Initial Filtration: Gases with low VOC concentration pass through a filter that retains solid particles harmful to the zeolite.
VOC Adsorption: Filtered gases pass through the rotor, where organic compounds are adsorbed onto the zeolite surface.
Clean Gas Emission: After VOC retention, the purified gases exit the rotor and are emitted into the atmosphere through a chimney.
VOC Desorption and Treatment
To regenerate the zeolite and release adsorbed VOCs, a small stream of hot gases is used in the opposite direction to the process gas flow. This procedure allows for:
The desorption of VOCs, obtaining a concentrated gas at a temperature of 50-60°C.
The possibility of treating this concentrated gas by thermal oxidation, generally in a thermoreactor.
System Energy Efficiency
Process gases passing through the rotor’s cooling sector emerge at a temperature of 75-110°C. This residual heat can be used to preheat the desorption air, thereby reducing the system’s total energy consumption.
Advantages of Using a Zeolite Rotoconcentrator
Reduced Energy Consumption: Minimizes the amount of gas to be thermally treated.
Increased VOC Capture Efficiency: Effective adsorption with less environmental impact.
Optimized Gas Treatment: Facilitates the subsequent thermal oxidation process.
Compliance with Environmental Regulations: Contributes to the reduction of pollutant emissions.
The use of a zeolite rotoconcentrator is an efficient and sustainable solution for industrial gas purification, allowing for reduced energy costs and optimized emission treatment processes.
Are you looking for an efficient solution to treat large volumes of air with low VOC concentrations?
Discover how a zeolite reconcentrator can optimize your treatment system.